INTEREUROPEAN Tire Building Machines: Uni-Stage, COMBI, and Traditional TBM Overview
This article introduces INTEREUROPEAN’s complete tire and rubber machinery lineup: Uni-Stage single-stage tire building machines, COMBI combined-stage TBMs, traditional first/second-stage TBMs, bead apexing lines, bias cutters, slitter lines, and air spring production equipment.
Keywords: tire building machine; TBM; Uni-Stage; green tire; bead apex; tire manufacturing equipment; COMBI TBM; air spring
1. Uni-Stage TBM (Single-Stage Tire Building Machine)
The next-generation fully automatic single-stage tire assembly machine uses Uni-Stage process technology, globally recognized and nominated for the 2015 Tire Technology International Innovation Excellence Award.
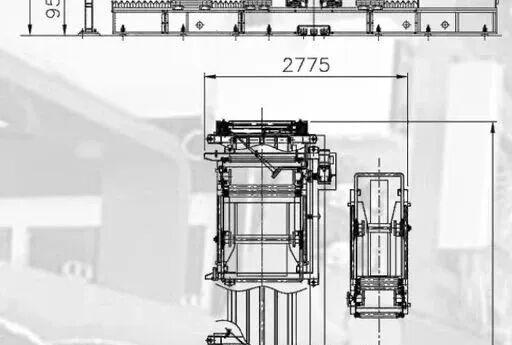
Uni-Stage TBM general assembly drawing
Key Configuration Features
- All rubber semi-components have active guiding/correction systems, automatic cutting and stitching. Flat-drum tire assembly process. Advanced HMI touchscreen control with recipe management and self-diagnostics.
- Robots mount beads into bead lock positioning; transfer rings automatically unload green tires from the Uni-Stage drum.
- Customizable: 1-ply / 2-ply carcass, steel/fiber chafer; in-line or off-line inner liner + sidewall pre-assembly; tread from roll or pre-cut lengths; independent sidewall application.
- Uni-Stage drums supplied by INTEREUROPEAN (bladder-type or mechanical turn-up) or adapted to customer’s existing standard drums.
- High-config model with double belt drum + double Uni-Stage drum achieves 30-second cycle time per tire.
- Optional off-line inner liner + sidewall pre-assembly line to reduce costs and increase output.
In fully automatic mode, cycle time ranges 30–35 seconds per tire depending on drum type and material feeding configuration.
Machine Body
- Inner liner and sidewalls can be applied separately on the building drum for maximum recipe design freedom. Independent sidewall feed with ultrasonic cutting and electronic guiding; adds only 5 seconds to cycle time.
- Bead + isolator ring cassettes come from the company’s proven apexing line. One apexing line serves 2 Uni-Stage machines as standard supply.
- Same robot places beads onto automatic bead lock mechanism during the work cycle.
- Carcass components (inner liner + sidewall composite, 1st ply, 2nd ply) are centered by active guiding systems, cut to length, and applied to the Uni-Stage drum.
- Inner liner + sidewall composite uses special ultrasonic cutting with adjustable angle for minimal-angle skew cuts to increase joint contact area and avoid air entrapment. Multiple roller discs exhaust air during application.
- Throughout assembly, the carcass remains on the same Uni-Stage drum. After turn-up, the drum moves to pre-shaping position; the transfer ring picks up the belt-tread assembly from the belt drum and applies it.
Belt & Tread Assembly Unit
Belt and tread assemblies are built in two steps on independent belt drums mounted on a rotating turret:
- New-generation belt feeder: magnetic conveyor splices belt ends from below; high-definition cameras provide active belt guiding; multiple electronic systems verify length for uniform circumference distribution.
- After belt application, a high-speed winding head immediately applies nylon cap ply spirals with tension control; all winding patterns are programmable in recipes.
- Tread is applied directly from roll; on-drum ultrasonic knife cuts the tread (7/8 cut) with near-invisible splice. Adjustable skew angles maximize splice contact area. Pressure-adjustable multiple roller discs stitch the tread; active guiding centers the tread before application.
- After tread application, the transfer ring carries the belt-tread assembly to the pre-shaped carcass; final shaping, dynamic rolling, and green tire unloading complete the cycle.
Fully Automatic Material Feed System
Each unwind station has two removable slide carriages. While the machine runs, operators can change rolls outside the station; switching carriages automatically splices material inside, minimizing downtime.
The modular control system uses Allen-Bradley or Siemens PLC with touchscreen HMI, recipe management, full alarm handling, and production statistics. Optional chafer, gum strip, and nylon cap ply feeds; various drum sizes; motor-adjustable belt drums; full range of transfer rings. All key process parameters are electrically recipe-driven: conveyor angle follows drum diameter, centering follows material width, rolling follows tire size — minimizing changeover time while maintaining flexibility and capacity.
Standard Configuration
- a. Rotary main frame with 2 Uni-Stage drums
- b. Component splice monitoring system
- c. Rotating turret with double belt drums covering all diameter ranges
- d. Mobile transfer ring with multi-segment sectors for full diameter range
- e. 3 laser positioning marking systems
- f. Multi-disc stitching rollers for exhaust
- g. Automatic bead lock ring; automatic bead loading robot
- h. Fully automatic carcass component feeder (2-ply capability, 4 unwind stations, active guiding, automatic length cutting, inner liner+sidewall pre-assembly, splice/wrinkle detection sensors, roll-present sensors, rigid vibration-damping frame)
- i. Fully automatic belt-tread component feeder (1st/2nd belt feeders with bottom splicing, double unwind each, active guiding, length verification, nylon cap winder with tension control, large accumulator, tread feeder with double unwind, multi-stage active guiding, on-drum ultrasonic tread cutting up to 15° skew, pressure-adjustable tread stitching, deformation/splice sensors)
- j. Green tire dynamic rolling device (all parameters recipe-driven; compatible with TOS/SOT structures)
ITAC Integrated Tire Assembly Unit (2.5 Million Tires/Year)
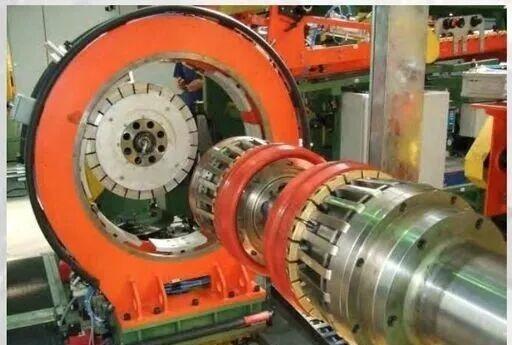
Uni-Stage TBM on-site view 1
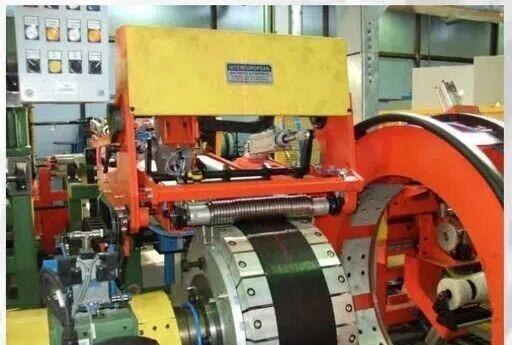
Uni-Stage TBM on-site view 2
The ITAC unit consists of:
- 4 fully automatic tire building machines
- 2 bead apexing lines
- 1 bead winding line
Capacity: 8,000 green tires/day, 2.5 million tires/year; can produce 4 different tire sizes simultaneously. Staffing: 6 operators total (1 per building machine, 1 shared between two apexing lines, 1 for bead winding).
Beads are wound in the dedicated in-unit bead line (square or hexagonal cross-section). Beads are automatically unloaded from the drum into cassettes, conveyed to the two apexing lines for apex extrusion and application. After apex application, robots load beads onto mobile carts separated by plastic isolator rings. Carts automatically transport to the 4 building machines. Buffer carts at each building machine inlet ensure 24-hour uninterrupted production. Each apexing line changes size every 12 hours or every 4,000 beads, and can supply two sizes to two machines simultaneously.
Bead manufacturing, apexing, and tire assembly are fully inspected by cameras and laser light curtains at every step. Automatic size changeover minimizes downtime. Four independent machines can each dedicate to specific sizes, only changing within the same bead diameter range — small-batch orders don’t cause major capacity loss.
ITAC can be configured as Uni-Stage or COMBI. Products: PCR passenger tires and LT light truck tires, up to 24 inches, including ultra-high-performance tires.
Uni-Stage TBM Technical Parameters
| Parameter | PCR-LT20 | PCR-LT24 |
|---|---|---|
| Bead diameter | 13–20″ | 15–24″ |
| Max green tire diameter | 800 mm | 1000 mm |
| Max bead setting width | 600 mm | 700 mm |
| Belt drum diameter | 750 mm | 980 mm |
| Max inner liner+sidewall width | 1000 mm | 1200 mm |
| 1st ply width | 900 mm | 1000 mm |
| 2nd ply width | 900 mm | 1000 mm |
| Max sidewall width | 240 mm | 260 mm |
| Belt width | 280 mm | 350 mm |
| Tread width | 350 mm | 450 mm |
| Tread length | 2500 mm | 3200 mm |
| Cycle time per tire | 30 s | 40 s |
| Max daily output* | ~2500 tires/day | ~2000 tires/day |
| Operators | 1 per machine | 1 per machine |
| Footprint (2-ply) | 12.5×12.9 m | 13.0×13.5 m |
*Output depends on operating conditions, operator skill, and equipment efficiency.
2. COMBI TBM (Combined First + Second Stage)
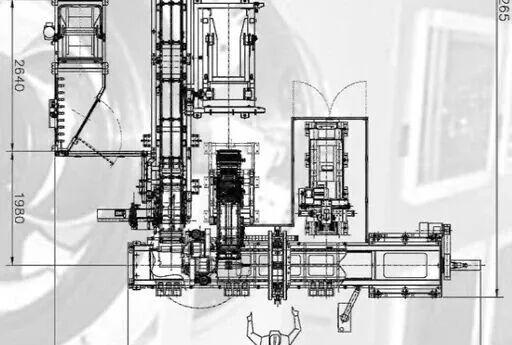
COMBI TBM drawing
The COMBI integrates first-stage and second-stage building into one fully automatic system:
- Cycle time: 35 seconds per tire; footprint: 11 m × 12 m
- Max daily output: 2,000 green tires; only 1 operator.
COMBI serves PCR passenger and LT light truck tires, integrating first and second-stage building into a single fully automatic machine — no manual intervention, one complete green tire every 35 seconds. The customer retains traditional two-stage process design freedom while gaining full automation. About 80% of the design derives from proven INTEREUROPEAN production equipment; the remaining 20% is custom-developed for this system. Timing analysis and 3D motion simulation ensure no wasted motion.
The machine has 5 parallel workstations, each with cycle time ≤35 seconds, sustaining one green tire every 35 seconds.
Workflow
- Station 1 (First-stage REC drum): Carcass components (inner liner, 1st ply, 2nd ply) are actively guided, cut to length, and applied to the REC drum. Inner liner uses adjustable-angle ultrasonic skew cut to avoid air entrapment. Multi-disc rollers exhaust air; side press wheels secure edges. Robot loads bead at cycle start for bead setting and turn-up. Second ply can be applied before or after turn-up for maximum design flexibility.
- Sidewall application station: Two independent ultrasonic knives apply and cut sidewalls on-drum (7/8 cut) with high splice precision; adjustable skew angles make near-invisible splices. Multi-disc rollers stitch; support idlers hold sidewall edges for uniform splices. Independent active guiding for both sidewalls. This station also performs final carcass rolling and automatic carcass unloading.
A dedicated transfer mechanism moves the carcass from first-stage drum to second-stage shaping drum without manual handling. The shaping drum receives the carcass and pre-shapes; the transfer ring brings the belt-tread assembly from the belt drum for application. The shaping drum has mechanical bead locking for precise bead positioning.
Belt-tread assembly is built on the rotating turret’s two independent belt drums, same process as the Uni-Stage machine: magnetic bottom splicing, HD camera active guiding, length verification, immediate nylon cap ply winding with tension control, tread from roll with on-drum ultrasonic cutting, multi-disc pressure-adjustable stitching. Final shaping, dynamic rolling, and green tire unloading complete the cycle.
COMBI Technical Parameters
| Parameter | COMBI-1320 | COMBI-1524 |
|---|---|---|
| Bead diameter | 13–20″ | 15–24″ |
| Max green tire diameter | 800 mm | 1000 mm |
| Max bead setting width | 600 mm | 700 mm |
| Belt drum diameter | 750 mm | 980 mm |
| Max sidewall width | 240 mm | 260 mm |
| Belt width | 280 mm | 350 mm |
| Tread width | 350 mm | 450 mm |
| Cycle time per tire | 35 s | 40 s |
| Max daily output* | ~2000 tires/day | ~1500 tires/day |
| Operators | 1 per machine | 1 per machine |
| Footprint (2-ply) | 11×12 m | 12×13 m |
3. Traditional First-Stage and Second-Stage TBMs
First-Stage TBM
Fully automatic first-stage building machine for PCR/LT tires. Active guiding, automatic cutting and application; finger-up + bladder turn-up; touchscreen monitoring with recipe management and fault diagnosis. Cycle time as low as 45 seconds. Operator performs visual inspection, removes built carcass at each cycle, and loads new beads. Customizable: 1/2 ply, steel/fiber chafer, sidewall from roll or cassette, gum strip pre-assembly.
| Parameter | Value |
|---|---|
| Bead diameter | 13–17″ (opt. 15–20″) |
| Drum width | 250–550 mm (opt. 250–600 mm) |
| Inner liner width | 720 mm (opt. 800 mm) |
| Carcass ply width | 720 mm (opt. 900 mm) |
| Max sidewall width | 240 mm (opt. 300 mm) |
| Cycle time | ~45 s |
| Operators | 1 |
| Footprint (2-ply) | 5.78×9.69 m |
Second-Stage TBM
Fully automatic second-stage building machine. Active guiding, automatic cutting; rotating turret with double belt drums for optimized tact; bead-lock shaping drum; tread from roll with ultrasonic cutting; optional nylon cap winder; touchscreen with recipe and diagnostics. Cycle time as low as 45 seconds. Transfer ring removes green tire.
| Parameter | Value |
|---|---|
| Bead diameter | 13–17″ (opt. 15–20″) |
| Shaping drum type | Bead-lock type |
| Max green tire width | 780 mm (opt. 800 mm) |
| Belt width | 250 mm (opt. 300 mm) |
| Belt cutting angle | 18–30° |
| Tread width | 300 mm (opt. 350 mm) |
| Belt drum diameter range | 450–720 mm |
| Cycle time | ~45 s |
| Operators | 1 |
| Footprint | 7.40×10.27 m |
4. Fully Automatic Bead Apexing Lines
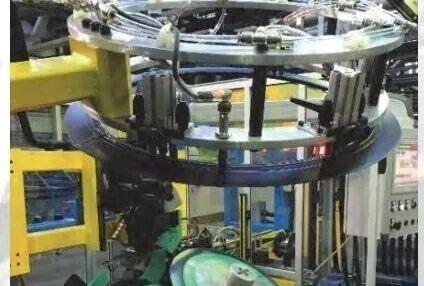
Bead apexing line robot loading
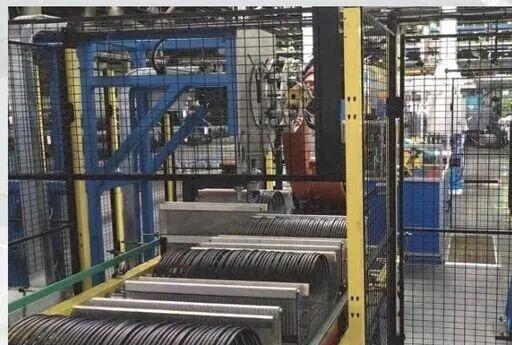
Bead apexing line overview
Available in PCR/LT version (13–22 inches) and TBR truck/bus version (17.5–24.5 inches). The new-generation fully automatic bead apexing line is based on multi-plant production experience. Key upgrades over previous semi-automatic models:
- Recipe-driven automatic size changeover
- Brushless motors with encoders (replacing photoelectric positioning)
- Highly synchronized stable splicing system
- 80 mm pin-barrel extruder for higher output on large beads
- Constant-speed extruder for stable apex cross-section
- Large-capacity tension accumulator
- Adjustable splice presser fingers for uniform splices
- Allen-Bradley PLC with remote diagnostics and MES integration
- On-line apex height and splice quality visual inspection with statistical processing
- Closed-loop chiller temperature control
- Optional KUKA robot for automatic bead loading/unloading and isolator ring insertion
PCR/LT version: cycle time ≤10 seconds per bead (~6 beads/minute), 1 operator per shift. TBR version: 90+90 mm dual cold-feed extruder, air cooling, 20 seconds per bead, footprint 25 m × 9.5 m.
5. Bias Cutter & Splicer Lines
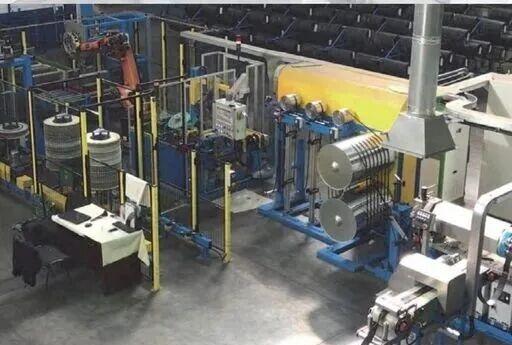
Bias cutter line
Fully automatic bias cutting and splicing line for steel and textile cord fabric. Cutting angle 40–90°; supports lap splicing and butt splicing. Includes unwind, accumulator, electronic centering, adjustable-angle knife, conveyor, and butt-splicing mechanism. Optional splice visual inspection, slitting, and rewind. Accuracy: splice tolerance ±0.5 mm; laser and CCD on-line monitoring. Output: variable-angle version up to 15 splices/minute; fixed 90° version up to 20 splices/minute.
6. Slitter Lines
Slitter line layout
Slits wide rubber sheets into narrow strips for cap ply gum strip application:
- Max raw width: 1000 mm; finished strip width: 20–300 mm
- Line speed: 0–30 m/min; multi-disc knife slitting; BST active edge guiding
- Width tolerance ±1 mm; max rewind roll diameter 600 mm
- Allen-Bradley PLC, FESTO pneumatics; footprint 6.65×2.03 m
7. Uni-Stage Air Spring Production Line
Air spring fatigue testing machine
Complete automated equipment for truck and bus air suspension springs: Uni-Stage air spring building machine, first-stage and second-stage air spring building machines, pressing machines, leak testers, dual-station curing presses, crimping presses, fatigue testing machines, bead winding lines, bias cutters, inner liner calendering/extrusion lines.
The Uni-Stage air spring building machine produces a complete green air spring every 20 seconds, max daily output 3,600 pieces; supports convoluted and cylindrical air springs. Factory host-system integration and remote diagnostics; double-slide unwinds for non-stop roll changes; 3 operators, estimated 30-minute size changeover.
8. Equipment Upgrade, Retrofit, and Custom Services
Uni-Stage TBM general assembly drawing
0
Uni-Stage TBM general assembly drawing
1
Uni-Stage TBM general assembly drawing
2. INTEREUROPEAN also supplies upgrade and retrofit packages for existing second-stage building machines, plus custom engineering services.